Modern mining depends on reliable conveyor and drive systems to keep material moving safely and efficiently. With 150 years of engineering expertise and local Australian support, RUD designs customised conveyor solutions that improve reliability, reduce maintenance and support emerging lower-emission mining and steelmaking technologies. The successful Vale briquette plant project demonstrates how engineered materials handling systems can help mining companies increase productivity while supporting decarbonisation initiatives.
For 150 years, RUD has been developing engineered chain technology and materials handling solutions that help mining companies maximise productivity, improve reliability and reduce maintenance. From open-cut mines to mineral processing plants, RUD's conveyor and drive systems are engineered to perform reliably in high load and abrasive environments where continuous operation is critical.
Beyond conveyor and drive technology, RUD supports the mining industry with lifting and lashing solutions, tyre protection and traction chains, engineered lifting solutions, heavy vehicle hoists and Australian engineering services. Together, these capabilities enable RUD to support customers across the entire mining lifecycle.
While RUD supports mining across many applications, efficient bulk material handling remains at the heart of modern mining operations. Every stage of the process depends on conveyor and drive systems that keep production moving safely and continuously.
Conveyor & Drive Systems Built for Mining
Every mining operation presents unique challenges. Material characteristics, production volumes, environmental conditions and site layouts all influence the type of conveying solution required.
RUD designs and manufactures conveyor and drive systems for horizontal, vertical and inclined conveying applications. RUD’s products include apron feeders, drag chain conveyors, bucket elevators, round steel chains and drive technologies such as TECDOS®, PI-GAMMA and OMEGA systems. Each system is developed to suit the specific material characteristics, throughput requirements and operating conditions of the site, helping maximise availability while reducing maintenance.
Every application is developed in collaboration with the customer instead of relying on standard designs. Backed by RUD's Brisbane engineering team, advanced manufacturing capabilities and in-house testing facilities, each solution is tailored to meet the operational demands of the site.
Supporting Lower-Emission Steel Production
As mining companies invest in lower-emission processing technologies, the performance and reliability of materials handling systems become even more critical. Conveyor systems must operate continuously under demanding conditions to keep production moving and protect the efficiency gains these new technologies are designed to deliver.
A recent example is Vale's innovative iron ore briquette plant in Vitória, Brazil. The new briquetting process eliminates the need for traditional sintering, one of the most energy-intensive stages of steel production. According to Vale, the technology has the potential to reduce greenhouse gas emissions during steelmaking by up to 10%, while also lowering emissions of sulphur dioxide (SOX) and nitrogen oxides (NOX).
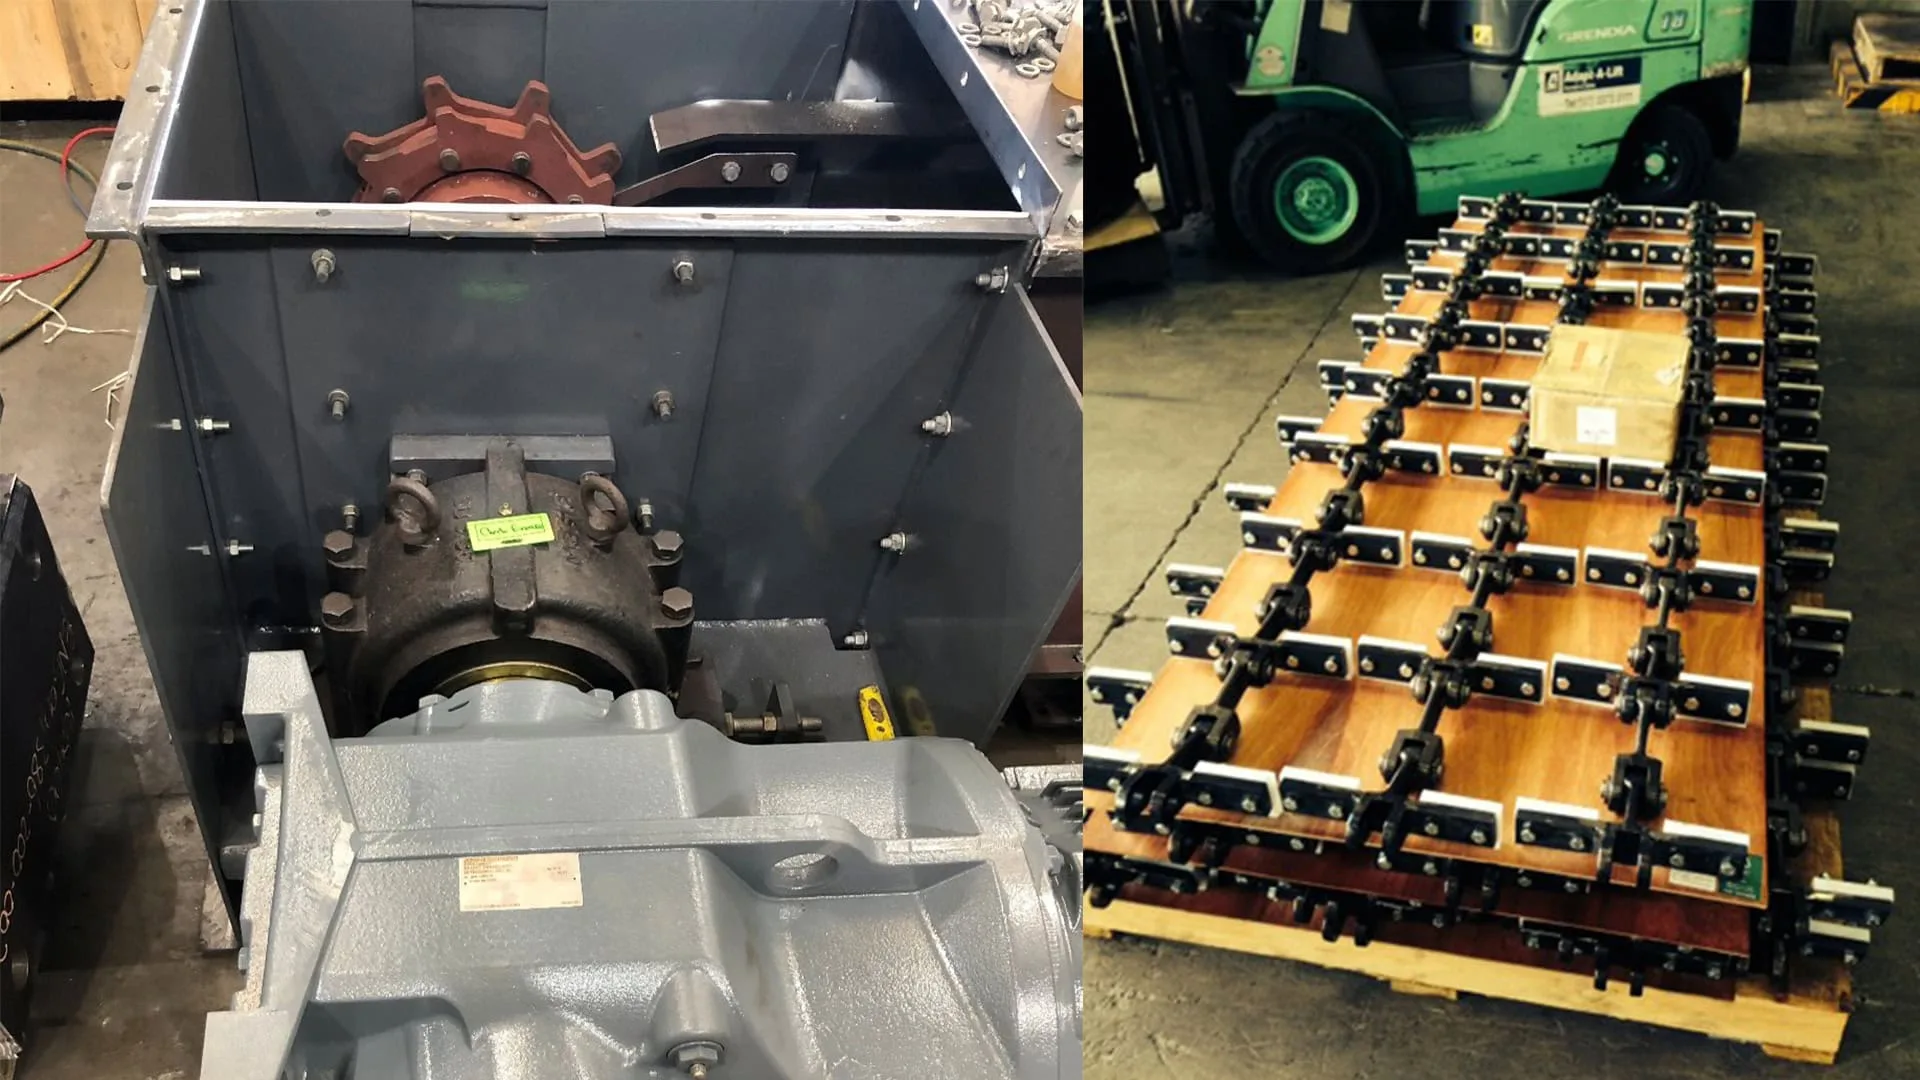
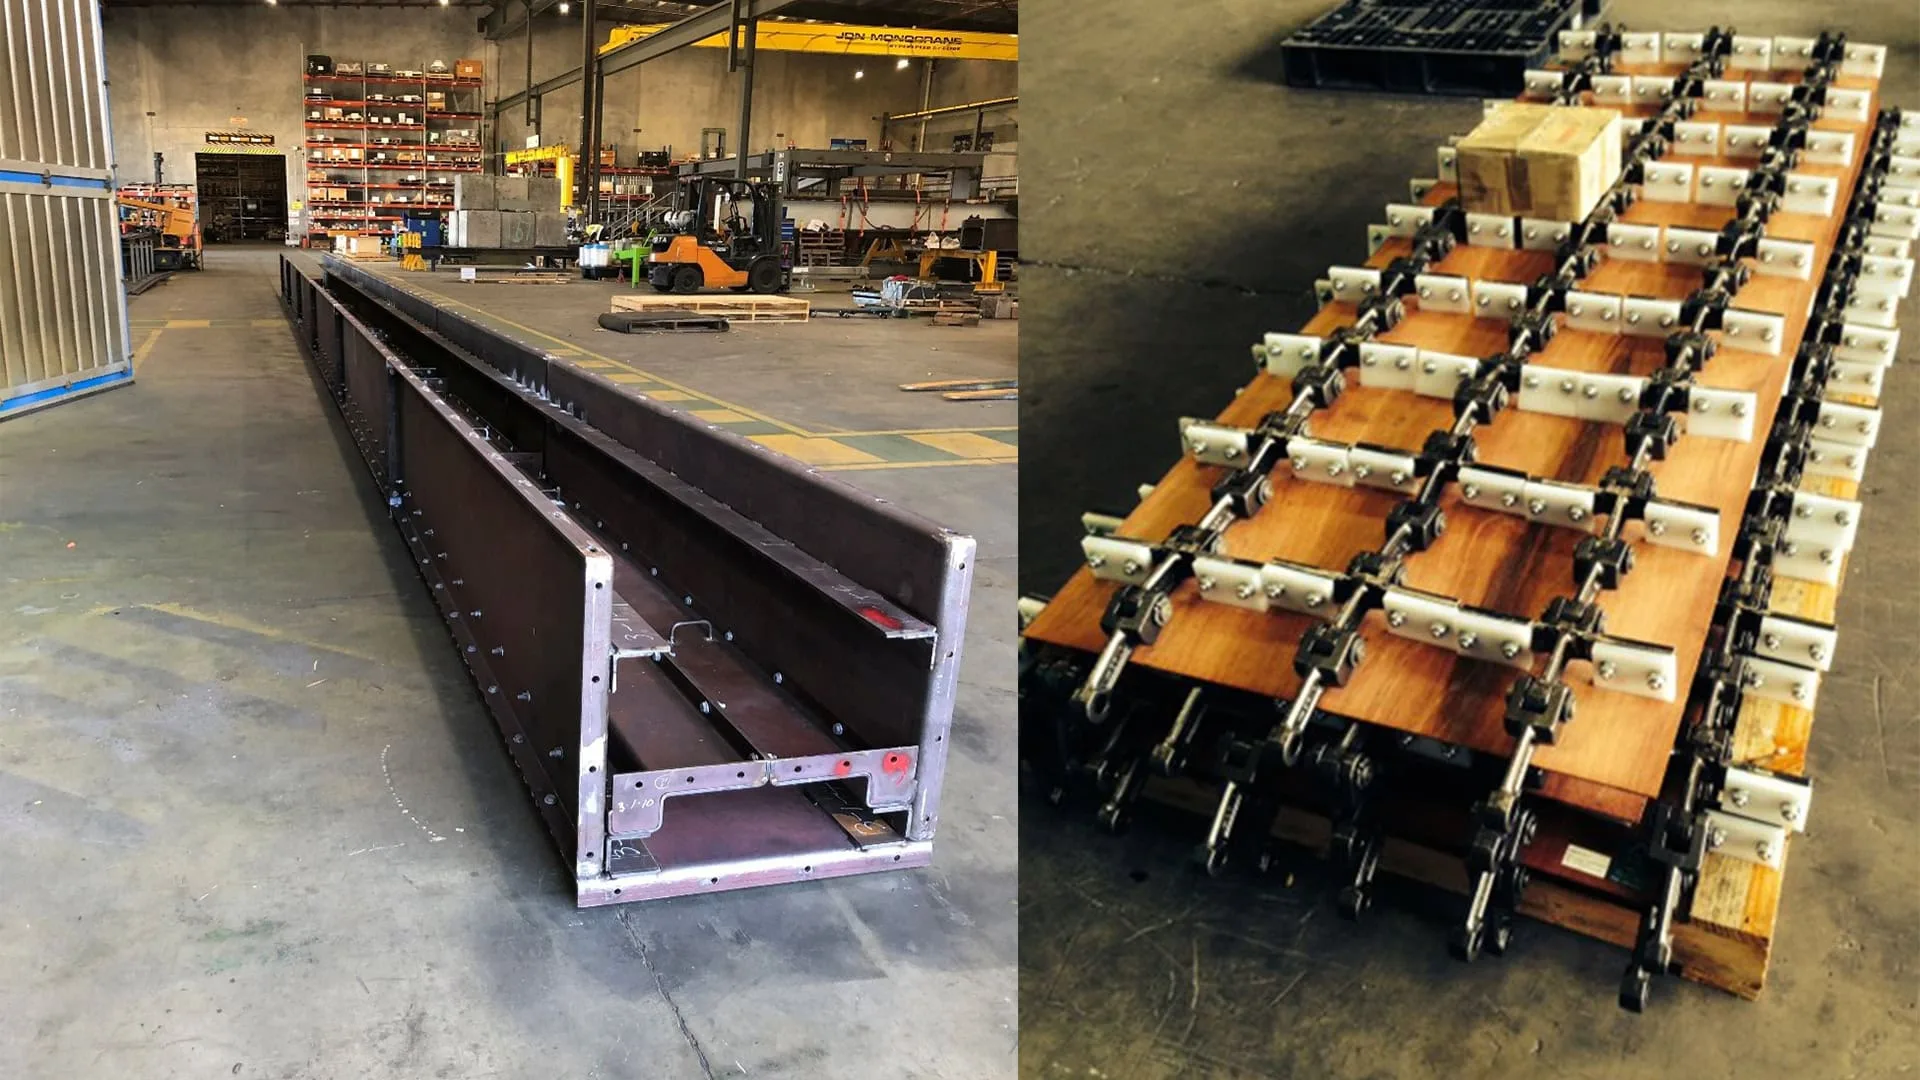
Supporting a plant of this scale requires more than innovative processing technology. It also depends on robust conveyor systems capable of moving large volumes of material safely and reliably throughout the production process. Working closely with the project team, RUD designed and manufactured six enclosed conveyors with capacities of 265 t/h and 485 t/h, engineered to withstand demanding operating conditions while delivering efficient, continuous material flow. Built using high-strength materials for maximum durability, the conveyor systems play an important role in maintaining reliable plant performance.
The Vale project demonstrates how advanced conveyor technology supports more than efficient material handling. It enables the successful implementation of next-generation processing technologies, helping mining and steel producers improve operational performance while reducing the environmental impact of steel production.
Engineering Expertise Backed by Local Support
Mining companies increasingly want partners who understand the complete materials handling process, from design and manufacture through to installation, maintenance and ongoing support.
With more than 40 years in Australia and 150 years of global engineering experience, RUD combines international expertise with local support. Its Brisbane based facility provides engineering, manufacturing, testing and technical services that help mining companies solve complex conveyor, drive and bulk materials handling challenges.
This integrated approach enables mining companies to improve safety, increase equipment availability and extend the service life of critical assets.
Keeping Mining Operations Moving
As mining companies continue to invest in automation, productivity and decarbonisation, the importance of reliable materials handling systems will only continue to grow.
RUD’s partnership with Vale highlights how engineered conveyor and drive solutions contribute to the success of innovative mining projects. The project demonstrates how engineering partnerships can help mining companies adopt new technologies while maintaining the reliability expected in demanding operating environments.
Whether transporting bulk materials through crushing circuits, processing plants or stockpiling operations, RUD's engineered conveyor and drive systems help mining companies improve reliability, maximise equipment availability and support the adoption of new processing technologies. Backed by Australian engineering expertise and 150 years of global innovation, RUD continues to deliver conveyor solutions built for the demands of modern mining.
Frequently Asked Questions
What conveyor and drive solutions does RUD provide for mining? RUD designs and manufactures customised conveyor and drive systems, including apron feeders, drag chain conveyors, bucket elevators, round steel chains and TECDOS®, PI-GAMMA and OMEGA drive technologies. Each solution is engineered to suit the site's material characteristics and operating conditions.
How do RUD conveyor systems improve mining operations? RUD conveyor systems help improve equipment reliability, maximise plant availability, reduce maintenance requirements and ensure the continuous movement of bulk materials through mining and mineral processing operations.
How is RUD supporting lower emission mining and steel production? RUD supported Vale's iron ore briquette plant in Brazil by designing enclosed conveyor systems that enable reliable material handling for an innovative steelmaking process with the potential to reduce greenhouse gas emissions by up to 10%.
For more details on our conveyor and drive solutions, email usor call us on 07 3809 1300.
This information is accurate at the time of publication, and RUD Australia takes no responsibility for any errors, inadvertent or otherwise. Some pictures are for illustration only.
Part 2 of the 2-part article.Click here to read Part 1.
RUD's manufacturing expertise includes a diverse range of conveyor and drive systems engineered for specific material handling challenges. Our objective is to provide perfectly coordinated systems, including individual components, that are high-performing, energy-efficient and require minimal maintenance. We understand that every minute of downtime costs money in industries like mining, power generation and recycling. Our systems are built to run continuously, reliably and safely.
We are known for our comprehensive range of chain-based conveyor systems. All our systems can be customised for specific materials handling as required. We use a variety of traction mechanisms, including round steel chains, forged link chains and high-tensile central chains. This versatility allows us to convey everything from fine powders to large, abrasive materials. Our bulk materials handling systems, such as the BULKOS conveyor, are specifically designed to face challenging and corrosive conditions in the fertiliser, potash, salt, and cement industries.
Our extensive range of specialised conveyor systems includes:
Drag Chain Conveyors: They are cost-effective and designed to convey materials horizontally or on an incline or in a combination of both. These systems are a go-to solution in all sectors, such as cement, fertilisers, power, steel and mining. They are built to manage high volumes of abrasive and hot materials with ease, ensuring continuous operation in harsh environments
Apron Feeder Conveyors: Found primarily in the mining and recycling industries, these conveyors feature overlapping, interlocking plates or aprons mounted on a chain. They are a crucial component for the precise and controlled feeding of primary crushers and screens, ensuring a smooth and consistent flow of material
Bucket Elevators: These elevators are an ideal solution for industries that require vertical transport. They provide a high-capacity, space-saving method for lifting materials to heights, commonly used in silos and bulk storage facilities
Screw Conveyors: These conveyors use a rotating helical screw blade to move granular materials or sludge within a compact space. They are often used for feeding materials at a controlled rate and can be configured to operate horizontally or on an incline
Beyond our product offerings, RUD provides a complete partnership experience. Our services include project planning, system commissioning and ongoing servicing. We collaborate closely with our clients from the initial concept phase to the final implementation, ensuring that the selected system perfectly matches their operational needs. This holistic approach, combined with our in-house manufacturing capabilities, is built to perform, built to last and built to solve the toughest conveying challenges in Australia.
RUD Australia celebrated 40 years in November 2024. From humble beginnings in 1984 in a garage on the south side of Brisbane to a 6000m2 facility in Larapinta QLD, including an office and warehouse in Perth, we have come a long way as one of the most trusted companies in the conveying, lifting, lashing and material handling industry.
If you want more details of our conveyor and drive systems, email us or call us on 07 3809 1300.
Article copyright to RUD Australia. This information is accurate at the time of publication, and RUD Australia takes no responsibility for any errors, inadvertent or otherwise.
This is a 2-part article.
For over 150 years, RUD has been a global leader in chains and conveyor technology. We leverage our extensive history and expertise to provide tailored, high-quality material handling solutions for Australian industries. With a state-of-the-art facility in Brisbane, we combine global knowledge with excellence in local manufacturing to ensure reliability and safety in every product.
Starting with humble beginnings as a blacksmith in 1875, the RUD group has expanded worldwide into chain technology innovations with a history of quality products. This innovative legacy has continued into RUD Australia, which operates from a state-of-the-art, 6,000m² facility in Brisbane, a testimony to Australian manufacturing and engineering excellence.
The Brisbane facility is a testament to RUD's commitment to local expertise and global standards. It is a fully integrated production hub designed to manage every stage of the manufacturing process, from raw materials to a finished, tested product. RUD Australia has invested in innovative technology which sets us apart from our competitors. Our production floor includes a SEVERT robotic welder with positional capabilities to ensure precision welds. This robot performs complex, repetitive welds with consistency, ensuring the structural integrity of every component. This is complemented by our advanced laser scanning capabilities, which allow our engineers to capture highly accurate 3D data of parts and assemblies. This precision is critical for quality control, reverse engineering and ensuring that every component fits together, reducing the risk of errors and costly delays.
Our commitment to quality extends beyond automation. Our highly qualified and experienced tradespeople bring expertise to our manufacturing process, allowing us to tackle custom and complex projects. By controlling the entire end-to-end process in-house, from design and manufacturing to assembly and testing, we can maintain a high level of quality control, minimise lead times, and ensure that every piece of equipment is built to exceed industry standards.
Our specialised engineering team is highly skilled and collaborative in every project. We share our knowledge, experience, insights, technical ability and best practices with other RUD subsidiaries around the world. This global knowledge network allows us to tap into a collective pool, optimising our processes to meet the unique and often challenging demands of Australian industries.
For example, a solution developed for a potash mine in Germany might be adapted and enhanced to solve a material handling problem in an Australian coal mine. This flow of information ensures that our clients benefit from the best of both local manufacturing and global expertise. This end-to-end flow in the design and manufacturing process minimises lead times and ensures reliability and safety for clients across the country, making RUD Australia a trusted partner for those who demand quality in every step.
RUD Australia celebrated 40 years in November 2024. From humble beginnings in 1984 in a garage on the south side of Brisbane to a 6000m2 facility in Larapinta QLD, including an office and warehouse in Perth, we have come a long way as one of the most trusted companies in the conveying, lifting, lashing and material handling industry.
To be continued ...
If you want more details of our conveyor and drive systems, email us or call us on 07 3809 1300.
Article copyright to RUD Australia. This information is accurate at the time of publication, and RUD Australia takes no responsibility for any errors, inadvertent or otherwise.
In today's dynamic industrial landscape, optimising operations and boosting efficiency are essential to any business's success. Robust conveyor systems are critical because they automate material movement, increase productivity, and potentially reduce operational expenditure. With diverse material handling solutions available, selecting the ideal conveyor for your specific requirements can be challenging. This comprehensive guide will help you with the insights needed to make an informed decision for your business.
Defining Your Conveyor System Needs
Before exploring the various options for industrial conveyors, such as chain or belt conveyors, it is essential to define your new system's role in your operations. Different types of conveyor systems are engineered for various purposes and performance criteria.
Consider these crucial questions:
Product Specifications: What materials or products will be conveyed? Factors such as size, weight, shape, temperature and material properties are essential to decide what you require
Throughput Requirements: What volume of material needs to be moved per unit of time? This dictates the required capacity of your automated conveyor system
Conveying Path and Length: What is the conveyor's overall distance and profile (horizontal, vertical, inclined)?
Facility Integration: How will the new system integrate with your existing machinery and the available confined space?
Budgetary Considerations: Conveyor technology ranges from low-budget setups to complex, feature-rich electro-mechanical solutions. Establish your budget and prioritise features accordingly
Understanding Diverse Conveyor System Applications
Once your operational needs are precise, let us explore various conveyor system types and their typical applications:
Single-Strand Drag Chain Conveyors: This is a cost-effective and adaptable choice, ideal for transporting lighter components, packages, or pallets along a flat plane. These are commonly used for general material transport
Double-Strand Drag Chain Conveyors: These systems offer enhanced stability and support, featuring two parallel strands, often with heavy-duty chain conveyor sprockets. They are ideal for heavier items, bulk materials handling and loads with uneven distribution, usually found in mining and bulk material industries
Chain Belt Conveyors: A specialised equipment designed to receive material discharged from trucks and convey it to a processing plant or other downstream equipment. It utilises a chain-driven belt system to handle a high volume of material and minimise spillage. These feeders are particularly useful in applications like quarries, terminals and mining operations
Central Chain Bucket Elevators: These are specifically designed for vertical movement of bulk materials such as grain, sand or aggregates. Buckets attached to a central chain efficiently scoop and lift materials
Round Link Chain Bucket Elevators: These are like central chain elevators but utilise round link chains for superior strength and durability in demanding, heavy-duty industrial applications
Apron Feeders: These heavy-duty conveyors feature overlapping, interlocking plates or aprons mounted on a chain. They are engineered for the precise and controlled feeding of bulk materials into processing equipment or conveyor lines.
Screw Conveyors: Designed for handling bulk materials horizontally or on an incline, using a rotating helical screw blade within a trough or tube to move granular or powdered solids
RUD Australia: World-Class Conveyor and Drive Systems
RUD is reputed worldwide as a leading conveyor manufacturer and provider of comprehensive material handling solutions in Australia. Our conveyor and drive systems are known for their reliability, design and low maintenance requirements, making them an ideal choice for industrial automation.
Durable Engineering: RUD uses premium-grade materials and innovative engineering processes to ensure our conveyor components and entire systems withstand rigorous, continuous operations and deliver a long service life
Customisable Solutions: RUD Australia also offers an extensive range of configurations and options for tailored conveyor technology to meet a company’s operational requirements. We can supply conveyor parts to complete, integrated systems
Reliable Performance: RUD’s commitment to quality translates into dependable performance, minimising downtime and reducing ongoing maintenance costs. Our drive technology systems are engineered for high performance for all material movements
Safety Excellence: Safety is critical in all RUD conveyor designs, incorporating features that protect both operators and the site, ensuring compliance with Australian safety standards
Comprehensive Service: RUD provides end-to-end expertise, encompassing engineering, project planning, system commissioning and ongoing servicing. We offer solutions from individual components and modules to entire turnkey systems, ensuring sustained operational reliability
Global Partnerships: We collaborate with international manufacturers such as Gambarotta and MCV to integrate our chains into their systems
Choosing the appropriate conveyor system is a strategic decision that empowers you to optimise your material flow and operational efficiency. By evaluating your needs and researching available conveyor solutions, you can be prepared to select the perfect fit for your business.
Interested in our conveyor system solutions? Call us on 07 3809 1300 or enquire here.
Copyright to RUD: This information is accurate at the time of publication, and RUD Australia takes no responsibility for any errors, inadvertent or otherwise.
The Australian cement manufacturing industry relies heavily on efficient material handling for its complex processes, from raw material extraction to the final product. This article explores the crucial role of material conveying equipment in enhancing productivity, safety, and sustainability within Australian cement plants and highlights RUD Australia's tailored solutions.
Cement extraction is a complex process that requires efficient management of various raw materials. Given the logistics of manufacturing and the sheer volume and weight involved, material handling equipment is an essential component in any cement plant.
Since material handling equipment is used throughout the cement process, from extracting limestone to moving bulk clinker, proper use can enhance productivity and simplify operations.
As an innovative technological trendsetter, RUD provides a range of material handling solutions and equipment that can withstand the challenging conditions of the cement industry.
Significance of Material Handling Equipment in Cement Production:
Material conveying requires the safe and efficient transportation of raw materials (mainly limestone, gypsum, and fly ash) and bulk products (clinker). The right equipment can ensure safety, decrease downtime and ensure compliance with environmental and industrial standards.
Types of Material Handling Equipment for Cement Production
Bucket Elevators
Bucket Elevators transport bulk materials vertically, such as powdered lime scale or clinker. They also transfer, lift, convey, and store materials between different levels using less space and a large volume. Based on the application, a suitable (Chain or Belt) bucket elevator can be selected.
Benefits of Bucket Elevators:
They can move bulk material vertically
They keep the materials moving between the phases of production
They are suitable for both powdery and fine granular material
Drag Chain Conveyors
Drag Chain Conveyors can transport a wide range of bulk materials. Their operation is based on the continuous movement of a chain placed in a rectangular section steel trough with a dust cover, coupled to a drive gear and sprockets/wheels. Although the material is usually dragged along the bottom of the trough by the lower section of the chain, it is also possible to convey material in the upper part. The drag chain conveyors from RUD are high quality, with sturdy construction, simple to set up for easy maintenance and reliable.
Benefits of Drag Chain Conveyors:
Built to withstand heavy loads and rigorous operating conditions
Can be tailored to specific application requirements, ensuring optimal performance
Optimised power consumption to reduce operational costs
Come with a closed dust dust-free operation which reduces pollution
Surface Feeders
Surface Feeders or Chain-Driven Belt Feeders are rubber belted pan feeders specially designed to convey materials discharged by trucks. These conveyors can receive a wide range of bulk materials, minimise spillage, and are suitable for quarries and terminals. They are available as a fixed or mobile option with dust covers.
Benefits of Surface Feeders:
Can receive a rapid flow of material from tippers or trucks and convey them to a hauling and processing plant with a controlled and adjustable flow rate
Since they only require a small ramp for the trucks, they are a lower investment compared to traditional feeders
Apron Feeders
Apron feeders consist of a chain equipped with interconnected pans moving at a controlled speed. They transport bulk materials like limestone, clay, and gypsum from storage bins or hoppers to crushers or other processes. Apron feeders are ideal for transporting large-sized, abrasive, and sticky materials, ensuring a steady and regulated flow of material throughout the production line.
Benefits of Apron Feeders:
Apron feeders are built to withstand harsh conditions and heavy loads, ensuring long-lasting performance and minimal downtime
They can handle a wide range of materials, including different particle sizes and moisture content
Apron feeders provide precise control over the material flow rate, preventing bottlenecks and optimising production processes
Tips to Make Material Handling More Efficient in Cement Plants:
If your business involves large material handling equipment fitted with sensors, control systems, and automation technology, it may be possible to automate and operate the system ‘hands-off’, reducing labour costs while keeping production efficient. Modern bulk material handling equipment is designed to be energy-efficient, using electricity instead of fossil fuels.
Conclusion:
Effective material handling is crucial for the efficiency and success of cement manufacturing plants. RUD Australia can implement ideal bulk material handling solutions that facilitate production workflows, reduce operational costs, and improve safety levels.
As the cement manufacturing industry continues to grow and adapt in response to industry demands, there is a need to upgrade material handling equipment and improve the use of industrial material handling tools. Effective processing procedures are critical for efficient production which meets the standards required for safety and quality. From robust bucket elevators to reliable conveyor belt scrapers, RUD Australia offers innovative solutions that drive efficiency and sustainability.
Article copyright to RUD: This information is accurate at the time of publication, and RUD Australia takes no responsibility for any errors, inadvertent or otherwise.